World's First Carbon-Neutral AAC Block & ALC Panel Smart Production Line Launched
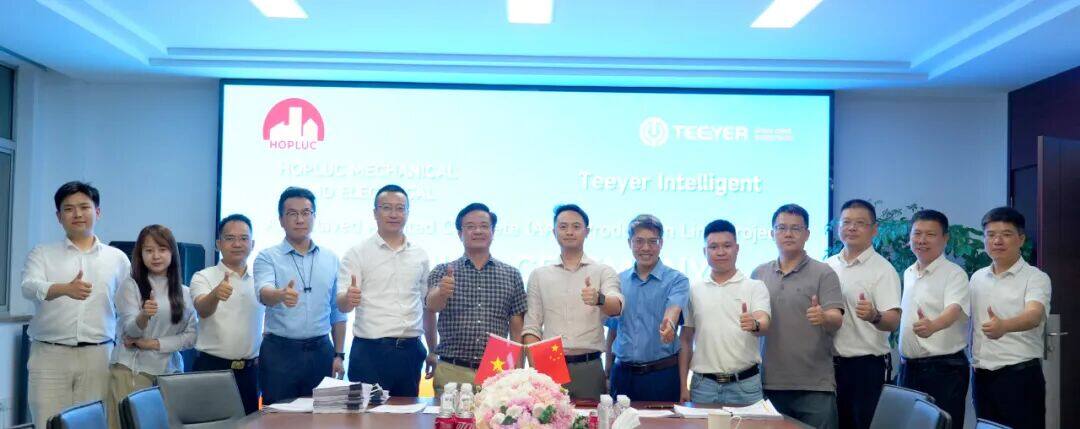
On June 11, 2026, Jiangsu Teeyer Intelligent Equipment Co., Ltd. signed a cooperation agreement with HOPLUC Construction Joint Stock Company, a leading industrial construction general contractor in Vietnam. The two companies will collaborate to build a modern, smart autoclaved aerated concrete (AAC) production base in Ninh Binh, Vietnam, and jointly elevate the green building materials industry in Vietnam and Southeast Asia to new heights.
Jointly Building a Modern AAC Smart Manufacturing Base in Ninh Binh, Vietnam
On June 11, 2026, Jiangsu Teeyer Intelligent Equipment Co., Ltd. and HOPLUC Construction Joint Stock Company, a leading industrial construction general contractor in Vietnam, signed a cooperation agreement. The two companies will collaborate to build a modern, smart autoclave-cured aerated concrete (AAC) production base in Ninh Binh, Vietnam, and jointly elevate the green building materials industry in Vietnam and Southeast Asia to new heights.
Located in Ninh Binh Province, Vietnam, the first phase of the project includes a production line with an annual capacity of 280,000 cubic meters of AAC blocks, designed for future expansion. Once fully completed, the facility will achieve an annual output of 450,000 cubic meters of AAC blocks or 300,000 cubic meters of AAC panels. The plant can flexibly adjust its product mix to meet market demand, helping to satisfy the growing need for green building materials in Vietnam and surrounding markets. Production is scheduled to officially begin in January 2027.
First Systematic Deployment of Next-Generation AAC Total Solution in an Overseas Project
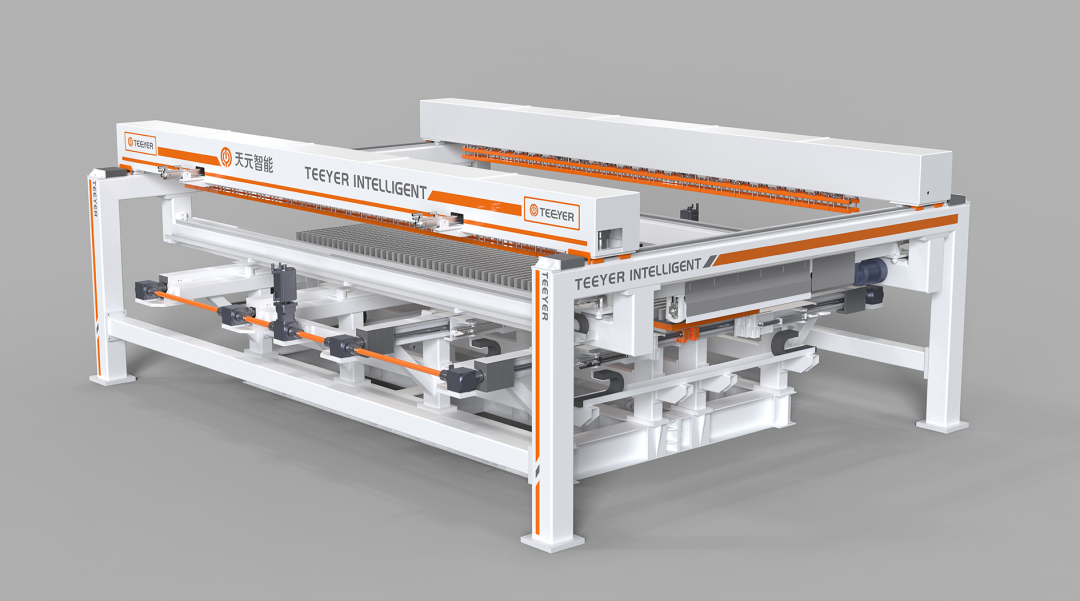
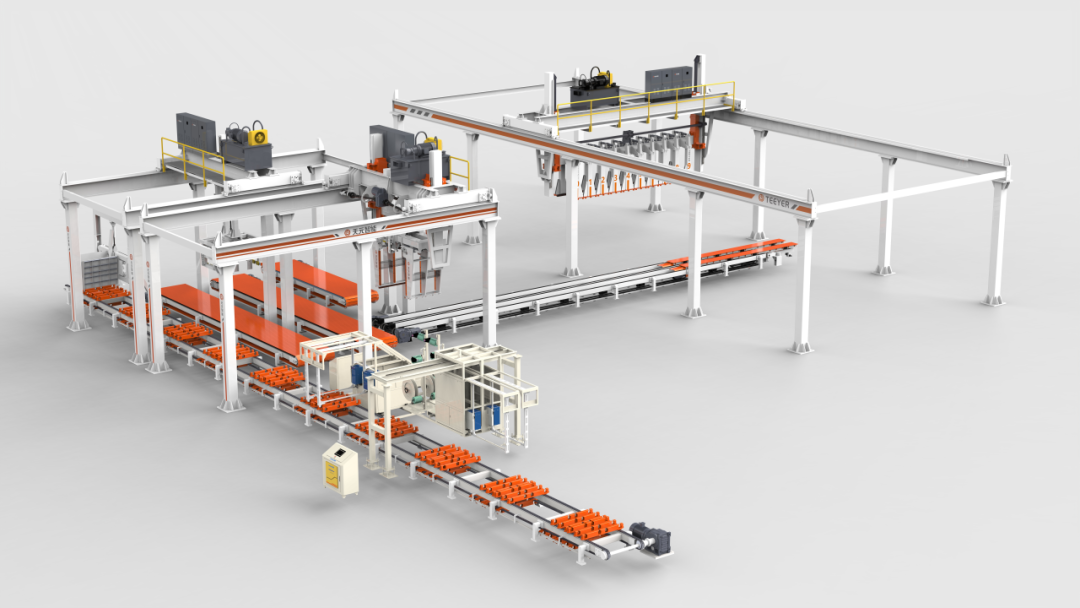
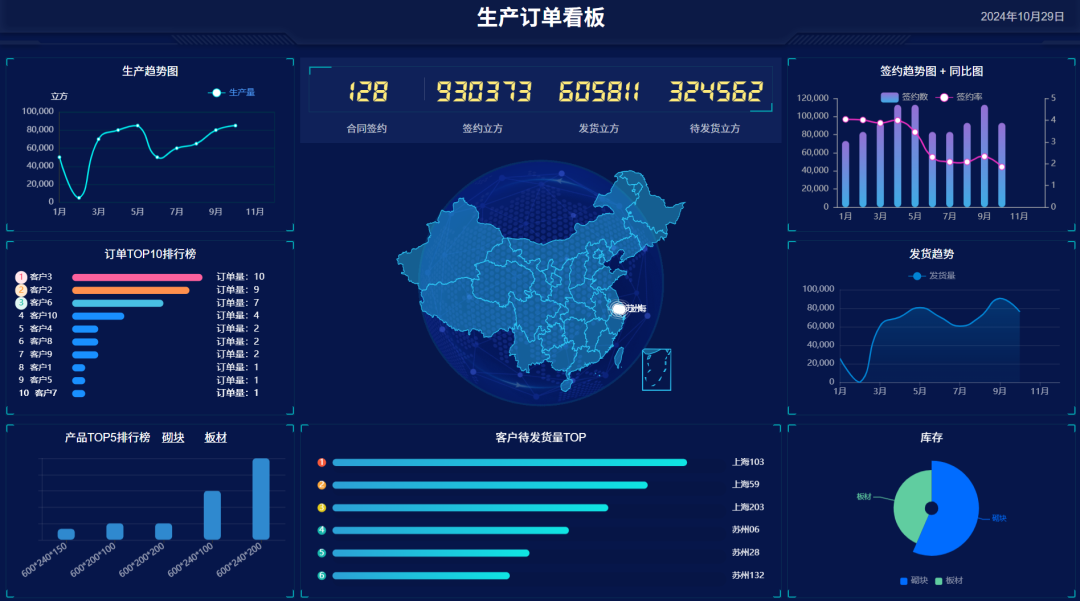
As the core equipment supplier and provider of the overall process solution, Teeyer Intelligent will deliver a complete AAC production line featuring smart equipment and automated control systems, along with multiple next-generation smart manufacturing technologies developed in-house. Notably, this project marks the first deployment in Vietnam of Teeyer Intelligent's bidirectional wet-splitting subsystem and pallet-free packaging system (supporting both palletized and pallet-free modes). By integrating these advanced technologies, the project will enhance product separation quality, packaging efficiency, and logistics flexibility—reducing operational costs and boosting production efficiency for the client. The project also includes a reserved interface for the Manufacturing Execution System (MES), laying a solid foundation for future smart factory construction and intelligent operational upgrades.
CarbonMiner and OCMC Technology Applications
Green and low-carbon principles were embedded in the project's design phase, with standardized interfaces for CarbonMiner's OCMC technology reserved. These technologies can be integrated later as needed, based on actual requirements and technological readiness, enabling future carbon reductions and green manufacturing enhancements to align with global construction industry sustainability trends.
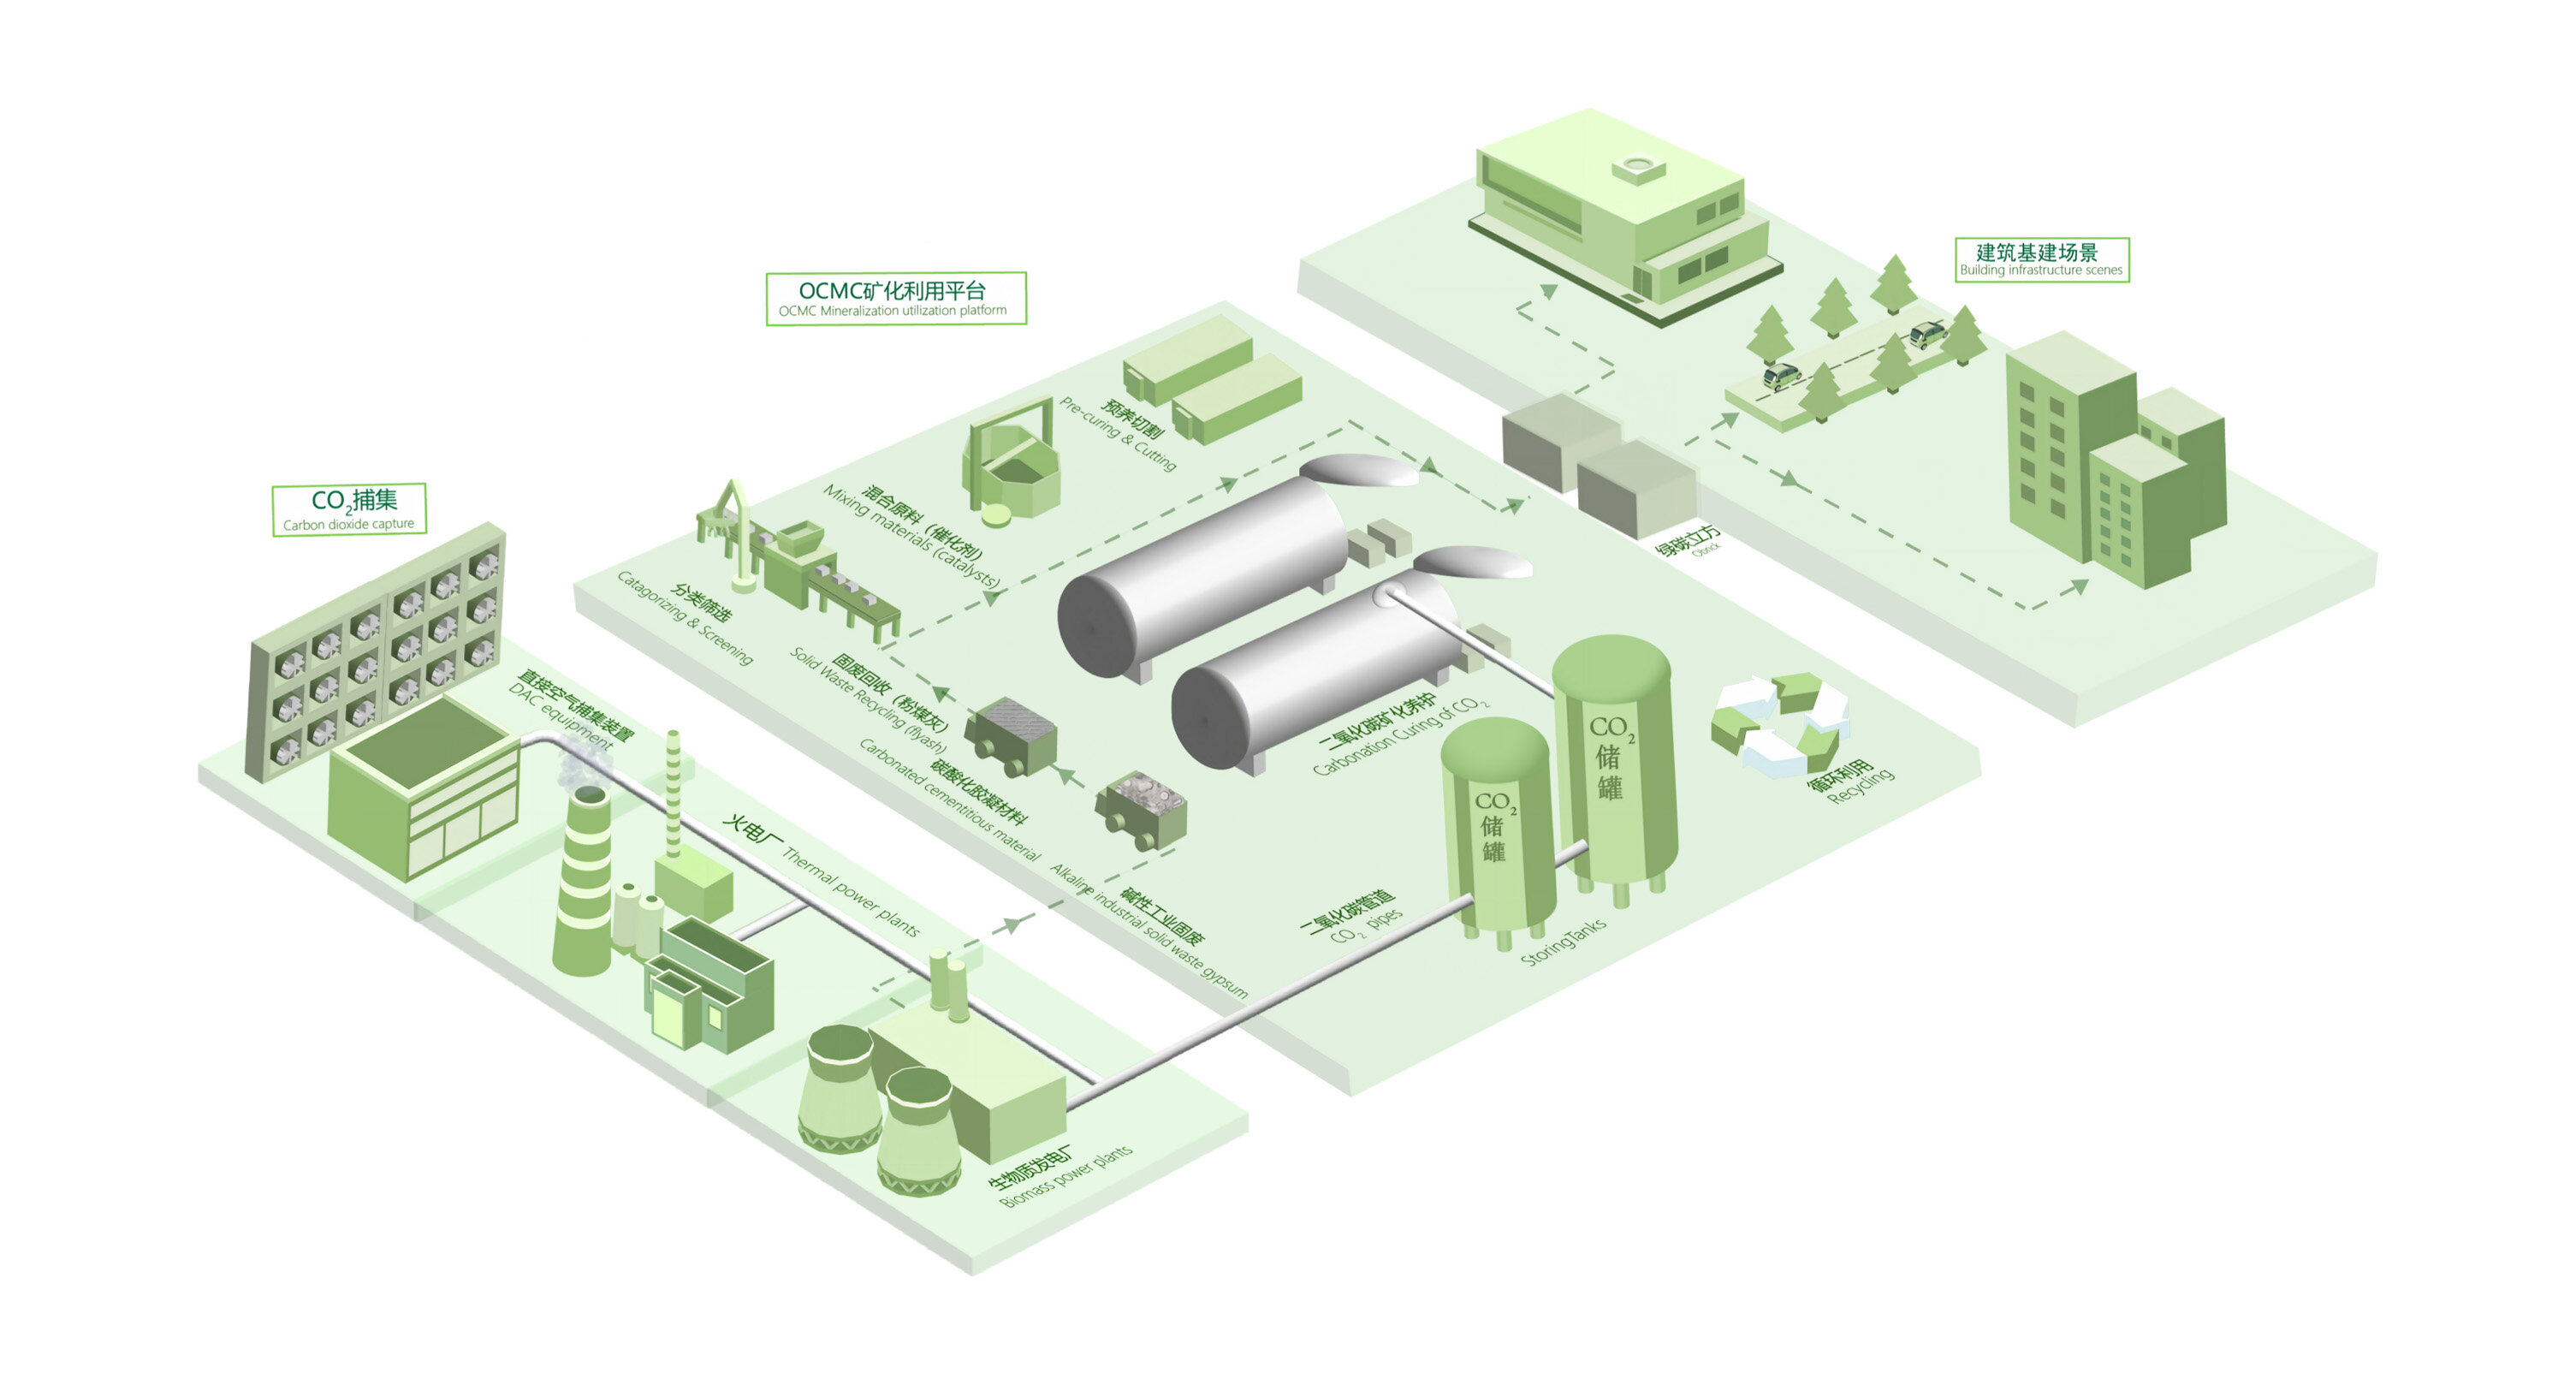
Omni Carbon Mineralization Concrete (OCMC)
CarbonMiner's OCMC technology simulates and accelerates natural rock weathering. Building on traditional autoclave-cured aerated concrete, it adds a CO₂ mineralization curing stage. Using specialized catalysts, dedicated equipment, and process controls, calcium and magnesium ions in cement-based raw materials react fully with CO₂. This forms stable, non-toxic, non-polluting carbonate crystals within the material matrix, permanently locking gaseous CO₂ inside finished products to prevent re-release—achieving source-level carbon sequestration.
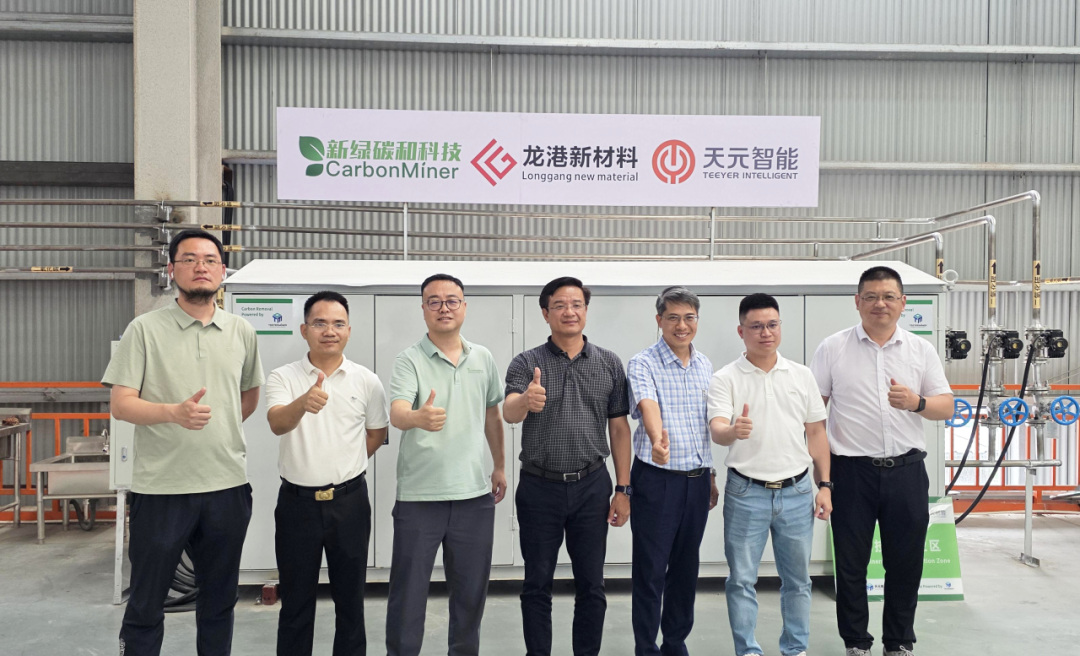
Vietnamese Clients Tour TeeyerMiner's Carbon Sequestration Production Line
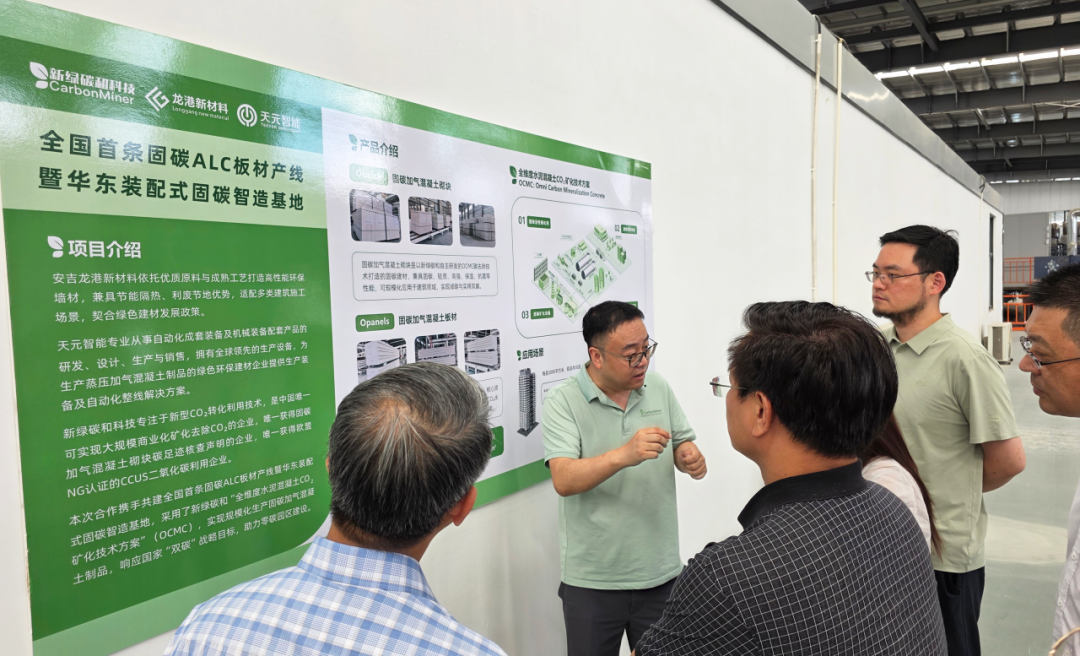
Introducing OCMC Technology to Vietnamese Clients
The World's First Newly Built Smart AAC/ALC Carbon Sequestration Production Line
This will be the world's first smart AAC/ALC manufacturing production line to integrate CarbonMiner's OCMC technology during the blueprint design phase.
Compared to traditional production line upgrades, this newly designed line delivers improvements across multiple dimensions: a more optimized layout, higher production efficiency, enhanced carbon sequestration performance, and stronger overall operational capabilities. By integrating world-class smart manufacturing equipment with carbon sequestration technology from the blueprint stage, this project creates deep synergy and unlocks new potential for carbon sequestration applications.
This implementation marks a new phase in TeeyerMiner's global expansion and signals that China's carbon sequestration technology is transitioning from domestic deployment to international adoption, delivering a Chinese solution to the global low-carbon industry.